ISO 11607 requires manufacturers to test worst-case scenarios across three areas—device configuration, sterile barrier manufacturing, and performance testing—to prevent packaging failures that compromise sterility and patient safety. Each worst-case definition is distinct and requires documented rationale to ensure medical device packages perform safely throughout their lifecycle.
- Worst-case device configuration means testing the product most likely to stress the packaging, such as the heaviest device or one with the most sharp features that could puncture or abrade.
- Worst-case sterile barrier manufacturing requires validating extreme pouch sizes and seal arrays within a product family, as process windows may be tighter at extremes than mid-range sizes.
- Worst-case performance testing demands sampling from multiple production lots or sealing at validated window extremes to capture the full range of package variation, not just average performance.
- Confusing process windows (machine settings) with specifications (finished package properties) leads to invalid validation that masks real-world risks.
- Documented rationale for each worst-case decision is essential evidence that manufacturers considered risk rather than dismissed it, protecting against recalls and patient harm.
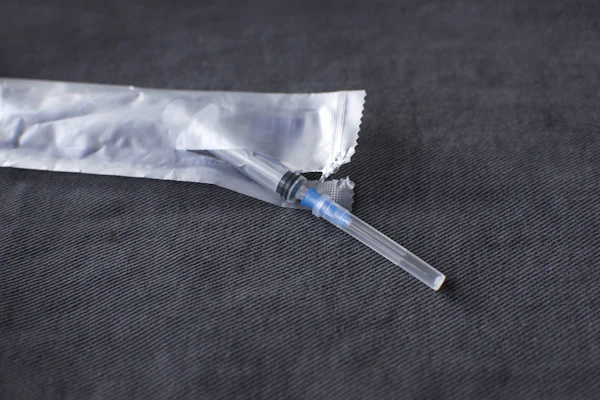
Packaging is considered part of the medical device, which means a packaging failure is a device failure. A compromised seal or punctured pouch can put sterility in doubt, trigger a recall, and most importantly put patient safety at risk. ISO 11607 exists to prevent those outcomes. Its repeated emphasis on "worst case" is where the standard becomes most practical and potentially confusing. In each of the three clauses that apply “worst case” it means something slightly different.
Worst Case Device Configuration
Under ISO 11607-1, Clause 6.1.9, when similar devices share a packaging system, the configuration that applies the most stress must be identified and used to determine compliance. Testing the lightest device in a product family while ignoring the heaviest says little about the product most likely to damage the package. Similarly, evaluating the number and type of fitments or sharp features that might puncture or abrade the package is important to determining the worst-case product. In some cases, that may mean that more than one device needs to be tested (e.g., the heaviest item and the one with the most fitments) to ensure that all devices across the product family will be properly protected.
Worst Case Sterile Barrier Manufacturing Process
Addressing the manufacturing process, ISO 11607-2, Clause 5.1.4 requires that worst-case configuration(s) of a sterile barrier system family be validated. For a family of chevron pouches all produced from the same materials, validating only a mid-sized pouch could mask problems that might be seen at the extremes. The process window may be smaller for the largest pouch or smallest pouches. When sealing multiple pouches at once, the array that has the greatest and least sealing areas should be considered. To ensure that the validation is meaningful for the entire sterile barrier system family, the worst-case configuration(s) for the (preformed) sterile barrier family must be carefully identified.
Packaging System Performance Testing
Performance testing under ISO 11607-1 Clause 8.2.2 carries perhaps the most subtle risk. The standard calls for testing the worst-case sterile barrier system together with the worst-case protective packaging, accounting for all specified sterilization processes and the most challenging contents. If the test packages do not represent the range of variation the process produces, results can look reassuring while hiding issues that will eventually reach the market. Sampling from multiple lots (typically three) helps capture the full range of package characteristics, such as seal strength, and is the most common approach. Alternatively, making seals at the extremes of the validated window (for example, using the lowest temperature, lowest pressure, and shortest dwell) offers a more conservative view, though at a higher cost.
Misunderstanding the standard creates risk in the opposite direction. Some manufacturers assume worst-case means producing packages at the extremes of the specification. Doing so generally requires operating outside the validated process window, which can create issues that would never occur in normal production. Because every process varies, some of those samples would likely fall outside the specification, producing misleading results.
Underneath all of this is a distinction that is easy to blur. A process window defines the machine settings used to make the package, while specifications define the properties of the finished package, such as dimensions, seal strength, and seal integrity. Confusing the two can lead to validation work that does not ultimately demonstrate the safety and efficacy of the package. ASTM F99 and F2559 are useful references for building meaningful specifications.
The common thread is documentation. Each worst-case decision, whether about device configuration, barrier system family, or test samples, must be supported by a documented rationale. That rationale is the manufacturer's evidence that risk was considered, not dismissed, and it should be be robust and adequately addresses potential risks.
In the end, worst-case thinking is a form of insurance. The effort to identify, test, and document the most demanding scenarios is modest compared with the cost of a recall, the loss of customer trust, or, more critically, harm to a patient. Manufacturers who treat ISO 11607's worst-case clauses as a risk-management tool, rather than a box to check, are far better positioned to keep their packaging, and their products, performing as intended.
To learn more, visit the Sterilized Packaging Manufacturers Council, an industry resource for best practices in sterile medical packaging manufacturing. More information on Worse Case Scenarios can be found in the FAQ section. https://www.sterilizationpackaging.org/